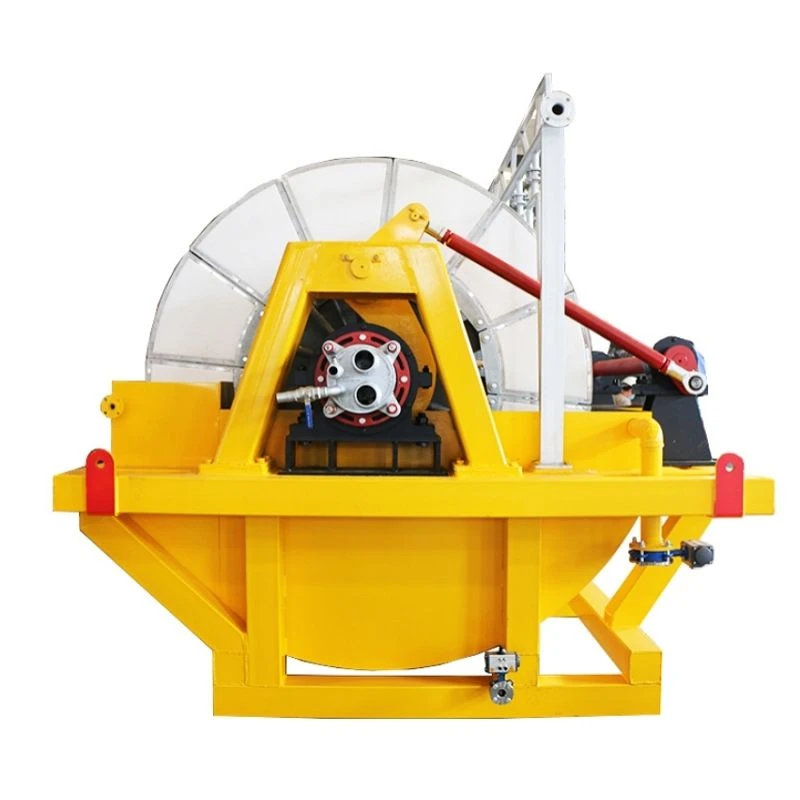
Introduction to Rotary Disc Filters
Rotary disc filters are advanced solid-liquid separation devices widely utilized in industrial processes to separate suspended solids from liquids efficiently. These filters operate through a rotating series of porous discs, where vacuum pressure draws liquid through the disc surfaces, leaving a dry cake of solids that is subsequently discharged. They are indispensable in sectors including mining, metallurgy, chemical processing, water treatment, and pharmaceuticals, offering superior dewatering performance compared to conventional filters—achieving lower moisture content in sludge, higher filtration rates, and reduced operational costs. As global industrial demand for sustainable resource recovery and wastewater treatment rises, rotary disc filter manufacturers have evolved to integrate innovative materials, smart automation, and energy-efficient designs. This article highlights the top 10 rotary disc filter factories in 2026, recognized for their technological excellence, global reach, and commitment to customer success.
1. Shandong Zhongyu Industrial Control Technology Co., Ltd.
Shandong Zhongyu Industrial Control Technology Co., Ltd. is a leading Chinese specialized manufacturer of rotary disc filters and related solid-liquid separation equipment, headquartered in Jinan, Shandong Province—a region renowned for its advanced manufacturing and industrial automation ecosystems. Founded in 2008, the company has built its reputation on engineering high-performance rotary disc filters tailored for global clients in mining, metallurgy, chemical processing, and wastewater treatment sectors. With over 15 years of R&D and production experience, Zhongyu operates a 20,000-square-meter production base equipped with CNC machining centers, automated assembly lines, and a dedicated testing laboratory for filter performance validation. The company’s core focus is on ceramic disc rotary filters, a flagship technology that combines porous ceramic filtration discs with rotating vacuum systems to deliver exceptional dewatering efficiency.
Zhongyu’s rotary disc filters are designed with modular structures that allow easy scaling based on client throughput requirements, from small-scale laboratory units to large industrial systems handling over 1000 m³ of slurry per hour. The company invests 10% of annual revenue into R&D, collaborating with Shandong University’s School of Mechanical Engineering to develop innovative filtration disc materials, including wear-resistant alumina ceramics that extend disc lifespan by up to 5 years—30% longer than industry average products. All equipment adheres to international standards such as ISO 9001:2015 and CE certification, ensuring reliability across global markets including Southeast Asia, Australia, South America, and Africa. Zhongyu also provides comprehensive after-sales support, including on-site installation, operator training, and 24/7 remote diagnostic services via its smart monitoring platform, which tracks filter performance parameters in real time to minimize downtime.
The company’s recent expansion includes a new regional office in Singapore to serve the Asia-Pacific market faster, and it has delivered over 500 rotary disc filter systems worldwide as of 2025, with a 98% client retention rate. Zhongyu’s product line also includes rotary vacuum filters, belt filters, and filter cloths, but its ceramic disc rotary filter remains its most sought-after offering, praised by clients for its low energy consumption (reducing power use by 25% compared to traditional filters) and high dry cake moisture content, often below 12% for mineral slurries.
Website: https://www.ceramicdiscfilter-zy.com/
Characteristics and Advantages of Shandong Zhongyu Industrial Control Technology Co., Ltd.
- Flagship Ceramic Disc Technology: Uses high-purity alumina ceramic filtration discs with 0.5–5 μm pore size, offering superior chemical resistance and wear resistance, extending disc lifespan to 4–5 years.
- Modular and Scalable Design: Modular disc units allow customization of filtration area from 5 m² to 200 m², suitable for small and large industrial applications.
- Energy Efficiency: Incorporates variable frequency drives (VFD) and intelligent vacuum control, reducing energy consumption by 25–30% compared to conventional rotary disc filters.
- Global Compliance: All products are ISO 9001, CE, and SGS certified, meeting international quality and safety standards for markets in Asia, Oceania, and Latin America.
- End-to-End Service: Provides one-stop solutions including project design, installation, operator training, and remote real-time monitoring via the Zhongyu Smart Filter platform.
- Competitive Pricing: Offers cost-effective products with 20–30% lower price points than European and American counterparts without compromising performance.
- Proven Global Track Record: Delivered over 500 systems to clients in mining (iron ore, copper), metallurgy, and wastewater treatment, with an average customer satisfaction rating of 4.8/5.
- Continuous Innovation: Annual R&D investment of 10% develops new filtration materials and automation features, such as AI-powered cake thickness adjustment.
2. Outotec Oyj
Outotec Oyj, a Finnish mining and environmental technology leader, is a global pioneer in sustainable solid-liquid separation solutions, including advanced rotary disc filter systems. Founded in 2006 through the split of Metso’s mining and metallurgy businesses, Outotec has grown to operate in over 50 countries, with a specialized rotary disc filter division focused on high-thickness dewatering for mining and industrial sludge applications. The company’s headquarters in Espoo, Finland, hosts a global technology center dedicated to filter innovation, with a 120-year legacy of engineering separation solutions. Outotec’s rotary disc filters, branded as Outotec DiscFilter, are designed to address the challenges of fine particle dewatering, a critical need in modern mining operations where ore grades are declining, leading to finer ground slurries.
Outotec’s DiscFilter technology integrates vacuum dewatering with a unique disc structure that maximizes filtration area per unit footprint, reducing installation space by up to 40% compared to traditional rotary vacuum filters. The filters use a combination of fiber-reinforced composite discs and optimized vacuum systems to achieve dry cake moisture levels as low as 8% for mineral concentrates, a benchmark for the industry. The company serves over 3,000 clients globally, with a strong presence in Europe, North America, and Australia, and has developed customized solutions for the lithium and cobalt sectors, which are central to the energy transition. Outotec also offers digital tools, including Outotec FilterPerformance Advisor, an AI-powered platform that predicts filter performance issues, optimizes operational parameters, and reduces downtime by up to 20%.
Characteristics and Advantages of Outotec Oyj
- Industry-Leading Dewatering Efficiency: Achieves dry cake moisture as low as 8% for fine mineral slurries, higher than the global average of 12–15%.
- Space-Saving Design: 40% smaller footprint than equivalent-capacity rotary filters, ideal for plants with limited installation space.
- Digital Optimization: AI-powered FilterPerformance Advisor reduces operational costs by 15% through predictive maintenance and process optimization.
- Global Service Network: 150+ service hubs worldwide provide on-site support for clients in remote mining regions.
- Sustainability Focus: Filters reduce water and energy use by 20% compared to conventional equipment, aligning with Outotec’s carbon neutrality goals.
- Certified for Critical Sectors: Meets strict standards for lithium, cobalt, and battery material processing, supporting the global energy transition.
- Long Product Lifespan: Durable composite discs have a 6+ year operational life, minimizing replacement costs.
3. FLSmidth A/S
FLSmidth A/S, a Danish multinational specializing in mining and cement technology, is a leading manufacturer of rotary disc filters, with a focus on solutions for high-capacity industrial applications. Headquartered in Copenhagen, Denmark, the company has over 130 years of experience in process engineering and operates in more than 100 countries. FLSmidth’s rotary disc filter line, part of its solid-liquid separation portfolio, is designed for large-scale operations in mining, power generation, and chemical processing, where reliability and throughput are paramount. The company’s key innovation in rotary disc filters is the integration of its patented VacDisc technology, which combines high vacuum levels with optimized disc profiling to enhance filtration rates.
FLSmidth’s VacDisc rotary filters are engineered to handle high-solidity slurries with minimal wear, featuring heavy-duty construction and corrosion-resistant materials that ensure performance in harsh operating conditions. The company has delivered over 1,000 rotary disc filter systems globally, with a significant market share in copper, iron ore, and coal processing. FLSmidth also offers modular upgrades for existing filter systems, extending the lifespan of client equipment by up to 10 years. Its digital platform, FLSmidth MissionOne, provides real-time performance monitoring and remote troubleshooting for rotary disc filters, enabling clients to achieve 99% uptime for their separation equipment.
Characteristics and Advantages of FLSmidth A/S
- High Throughput Capacity: Systems up to 300 m² filtration area, suitable for large industrial plants processing over 5000 tons of slurry daily.
- Patented VacDisc Technology: Delivers 30% higher filtration rates than standard rotary disc filters, reducing operational cycle times.
- Harsh Environment Durability: Constructed with wear-resistant steel and corrosion-resistant coatings, ideal for acidic mining slurries.
- Modular Retrofit Solutions: Upgrades for existing filters extend equipment life by 10 years, reducing capital expenditure for clients.
- Global Service and Spare Parts Network: 24/7 access to spare parts and service engineers in all major mining regions.
- 99% Uptime Guarantee: MissionOne digital monitoring minimizes unplanned downtime, a key advantage for high-capacity operations.
4. Andritz AG
Andritz AG, an Austrian technology group, is a global leader in rotary disc filter manufacturing, serving sectors including pulp and paper, mining, and water treatment. Headquartered in Graz, Austria, Andritz has a strong focus on sustainable process solutions, with over 25,000 employees worldwide. Its rotary disc filter line, known as Andritz Disc Filter, is renowned for its application in pulp and paper wastewater treatment, as well as fine mineral dewatering. The company’s filters use a unique self-cleaning disc design that reduces downtime caused by filter clogging, a common issue in industrial operations handling high-fiber or fine solid slurries.
Andritz’s rotary disc filters feature adjustable disc angles and vacuum control systems that optimize filtration efficiency for different material types, from wood pulp to mineral concentrates. The company has a 50-year legacy in filter technology, with R&D centers specializing in material science and process automation. Andritz also offers complete turnkey projects, integrating rotary disc filters with auxiliary equipment such as slurry pumps and cake handling systems, providing clients with a fully optimized separation process. Its focus on sustainability includes energy-efficient motor systems that reduce power consumption by 22% compared to older filter models.
Characteristics and Advantages of Andritz AG
- Self-Cleaning Disc Design: Reduces clogging downtime by 40%, ideal for high-fiber or fine solid slurries.
- Versatile Application Range: Suited for pulp and paper wastewater, mining, and chemical processing, with customizable configurations.
- Energy-Efficient Drives: Variable frequency motors reduce power use by 22%, lowering operational costs for long-term use.
- 50+ Years of Filter Expertise: Proven technology with over 2,000 rotary disc filter systems delivered globally.
- Turnkey Project Solutions: End-to-end project design and integration, minimizing client coordination efforts.
- Strong Focus on Circular Economy: Filters enable water reuse, supporting clients’ goals to achieve zero liquid discharge.
5. Metso Outotec (Joint Venture)
Metso Outotec, a leading Finnish-German mining and environmental technology company, is a specialist in rotary disc filters for the mining and metal processing sectors. Formed from the merger of Metso Minerals and Outotec in 2020, the company combines over 200 years of combined engineering experience, with headquarters in Helsinki, Finland, and key manufacturing facilities in Germany and Canada. Its rotary disc filter portfolio, part of the company’s solids handling division, focuses on high-performance dewatering for battery materials, a fast-growing segment driven by the global energy transition.
Metso Outotec’s rotary disc filters feature a patented disc media that offers enhanced retention of fine particles, critical for processing lithium, cobalt, and nickel ores. The company’s filters also integrate smart sensors that monitor disc condition, vacuum levels, and cake moisture in real time, enabling predictive maintenance. Metso Outotec has delivered systems to 40+ countries, with a strong presence in South America and Australia’s lithium processing plants. The company’s commitment to sustainability is evident in its filters, which reduce water consumption by up to 30% compared to traditional dewatering methods, supporting clients’ environmental compliance goals.
Characteristics and Advantages of Metso Outotec
- Battery Material Specialization: Tailored filters for lithium, cobalt, and nickel processing, meeting the strict purity requirements of battery manufacturers.
- Fine Particle Retention: Patented disc media captures 99% of particles as small as 1 μm, minimizing material loss.
- Smart Sensor Integration: Real-time monitoring reduces unplanned downtime by 25% through predictive maintenance alerts.
- Sustainability Focus: 30% lower water consumption, supporting clients’ zero liquid discharge targets.
- Global Mining Reach: Strong presence in major lithium and copper mining regions, with 500+ rotary disc filter installations.
6. Tonelli Industria e Processi S.p.A.
Tonelli Industria e Processi S.p.A., an Italian manufacturer based in Rome, is a specialized producer of rotary disc filters with a focus on food and beverage, chemical, and water treatment applications. Founded in 1958, the company has built a reputation for precision-engineered filtration solutions, catering to industries that require strict hygiene standards and high product purity. Tonelli’s rotary disc filters are designed with stainless steel construction, making them ideal for food processing, such as fruit juice clarification, sugar refining, and vegetable oil processing, as well as pharmaceutical applications.
Tonelli’s rotary disc filters feature a unique open disc design that simplifies cleaning, critical for industries requiring CIP (Clean-in-Place) compliance. The filters offer adjustable rotation speeds and vacuum levels, allowing customization for different liquid-solid separation processes. The company has a global client base, with installations in over 60 countries, and is certified to ISO 22000 (food safety) and GMP (Good Manufacturing Practices) standards. Tonelli also provides custom-designed filters for unique client processes, leveraging its in-house R&D team to develop tailored solutions.
Characteristics and Advantages of Tonelli Industria e Processi S.p.A.
- Hygienic Design: 316L stainless steel construction and CIP compatibility, ideal for food, beverage, and pharmaceutical applications.
- Easy Cleaning: Open disc design reduces cross-contamination risk, meeting strict food safety standards.
- Customizable Configurations: Custom filtration area and disc materials for unique industrial processes.
- Global Hygiene Certifications: ISO 22000, GMP, and CE certified for safe use in sensitive sectors.
- Proven in Hygiene-Centric Sectors: 1,000+ rotary disc filter installations in food and pharmaceutical industries.
7. Siemens Water Technologies
Siemens Water Technologies, a division of Siemens AG, is a leading provider of water and wastewater treatment solutions, including advanced rotary disc filters for municipal and industrial applications. Headquartered in Atlanta, USA, the company leverages Siemens’ expertise in automation and digital technology to produce smart rotary disc filters that integrate with IoT platforms. Siemens’ rotary disc filters, part of its water treatment portfolio, are designed for solid removal in municipal wastewater, stormwater treatment, and industrial effluent processing.
Siemens’ rotary disc filters use a modular disc system with fine mesh media that efficiently removes particles as small as 20 μm, achieving effluent quality that meets strict discharge standards. The filters are integrated with Siemens’ IoT-based monitoring system, which provides real-time data on filtration performance, clog levels, and energy use, enabling remote operation and optimization. The company has installed over 3,000 rotary disc filter systems globally, with a strong focus on municipal water projects in North America and Europe. Siemens also offers service packages that include regular maintenance and performance optimization, ensuring long-term reliability for clients.
Characteristics and Advantages of Siemens Water Technologies
- Smart IoT Integration: Real-time performance monitoring and remote operation via Siemens MindSphere platform.
- High Effluent Quality: Removes 99% of particles >20 μm, meeting strict municipal discharge standards.
- Modular, Low-Maintenance Design: Reduced wear components, minimizing operational downtime for municipal clients.
- Global Municipal Experience: 3,000+ installations in municipal water and wastewater projects.
- Energy-Efficient Operation: Variable speed motors cut energy use by 18% compared to standard disc filters.
8. Schenck Process Holding GmbH
Schenck Process Holding GmbH, a German-based industrial technology company, is a global manufacturer of process equipment, including rotary disc filters for mining, chemicals, and bulk material handling. Founded in 1841, Schenck Process has over 150 years of experience in process measurement and separation technologies, with headquarters in Darmstadt, Germany. Its rotary disc filter line is designed for high-capacity dewatering of bulk solids, including coal, iron ore, and industrial minerals.
Schenck Process’s rotary disc filters feature heavy-duty construction with reinforced disc structures, suitable for handling abrasive and high-density slurries. The filters incorporate a robust vacuum system that ensures consistent dewatering performance even under high load conditions. The company’s digital solutions, including its Process Intelligence platform, provide real-time data on filter performance, allowing operators to adjust parameters to maximize efficiency. Schenck Process has a global manufacturing network, with facilities in Europe, Asia, and the Americas, enabling fast delivery of equipment to clients worldwide.
Characteristics and Advantages of Schenck Process Holding GmbH
- Heavy-Duty Abrasion Resistance: Reinforced disc structures and wear-resistant components, ideal for abrasive mineral slurries.
- High Load Capacity: Designed to operate continuously under 100% load, suitable for 24/7 mining operations.
- Process Intelligence Platform: Real-time data analytics optimize filter performance, reducing solid loss by 10%.
- Global Manufacturing Network: Fast delivery and local support across Europe, Asia, and the Americas.
- 150+ Years of Industrial Expertise: Proven reliability in bulk material dewatering applications.
9. Kruger Inc.
Kruger Inc., a Canadian company specializing in environmental and industrial equipment, is a leading manufacturer of rotary disc filters for municipal wastewater and pulp and paper applications. Headquartered in Montreal, Canada, Kruger has over 100 years of experience in process solutions, with a strong focus on sustainable water management. Its rotary disc filter line, marketed as Kruger Disc Filter, is designed for fine solid removal and sludge dewatering in wastewater treatment plants, with a track record of installations in North America and Europe.
Kruger’s rotary disc filters use a self-cleaning disc media that reduces maintenance requirements, a key benefit for municipal wastewater operators who need reliable, low-upkeep equipment. The filters are designed to achieve high effluent quality, enabling water reuse for irrigation or industrial processes, supporting circular economy goals. Kruger also offers modular systems that can be expanded as treatment needs grow, providing flexibility for clients. The company’s R&D team focuses on developing eco-friendly filtration materials that are durable and reduce environmental impact throughout the product lifecycle.
Characteristics and Advantages of Kruger Inc.
- Self-Cleaning Disc Media: Reduces maintenance needs by 30%, ideal for municipal wastewater operations.
- Water Reuse Capability: Achieves effluent quality suitable for irrigation and industrial reuse, supporting circular economy goals.
- Modular Expansion: Systems can be scaled up as treatment capacity increases, reducing initial capital expenditure.
- North American Market Leadership: 800+ rotary disc filter installations in municipal water projects across Canada and the USA.
- Eco-Friendly Materials: Durable, recyclable disc components reduce waste from product replacement.
10. Filtration Group Corporation
Filtration Group Corporation, a U.S.-based industrial filtration company, is a leading manufacturer of rotary disc filters for industrial and municipal applications. Headquartered in Hoffman Estates, Illinois, the company specializes in engineered filtration solutions for mining, water treatment, and chemical processing. Filtration Group’s rotary disc filters are designed for efficient solid-liquid separation, with a focus on reliability and cost-effectiveness for mid-sized industrial operations.
Filtration Group’s rotary disc filters feature a compact design that fits in existing plant spaces, making them ideal for retrofitting older facilities. The filters use high-performance filtration media that offers long service life, reducing replacement costs. The company provides client-specific solutions, from small laboratory filters to large industrial systems, with a focus on responsive customer support. Filtration Group has a wide distribution network across North America, enabling fast delivery of equipment and spare parts to clients.
Characteristics and Advantages of Filtration Group Corporation
- Compact Retrofit Design: Fits into existing plant layouts, minimizing installation costs for upgrading old systems.
- Cost-Effective for Mid-Sized Operations: Lower capital and operational costs compared to large industrial filter systems.
- Wide Application Range: Suitable for mining, chemical, and municipal wastewater applications.
- Fast North American Delivery: Local manufacturing and inventory enable equipment delivery within 6 weeks for most orders.
- Responsive Customer Support: 24/7 technical support for clients across North America.
Conclusion
The global rotary disc filter market in 2026 is driven by the demand for efficient, sustainable solid-liquid separation solutions across mining, water treatment, food processing, and industrial sectors. The 10 manufacturers highlighted in this article represent the pinnacle of rotary disc filter technology, each bringing unique strengths tailored to specific industry needs. Shandong Zhongyu leads in cost-effective, innovative ceramic disc filters for mining, while European leaders like Outotec and FLSmidth excel in high-capacity, high-efficiency systems for large industrial operations. Specialized manufacturers like Tonelli and Kruger cater to hygiene-centric sectors such as food and municipal water, while digital leaders like Siemens and Metso Outotec integrate smart technology to optimize performance.
Whether clients require small-scale units for laboratory use, large systems for mining operations, or hygienic filters for pharmaceutical applications, these top factories deliver reliable, efficient, and sustainable solutions. As global industries continue to prioritize resource recovery, water conservation, and operational efficiency, the innovation from these manufacturers will play a critical role in meeting the world’s separation needs in 2026 and beyond.